Engineering Control of Sunscreen Spray Filling Precision: Achieving ±0.5g Tolerance via Valve Pre-tightening and In-line Weighing SOP

Updated: Sep 17
In the 2026 global sunscreen and personal care market, sunscreen sprays (especially high-pressure aerosols and dual-chamber pump bottles) have firmly secured their position as the "profit drivers" for brand owners expanding overseas, thanks to their ultimate reapplication experience. However, behind the carnival of high-speed mass production (e.g., 200-400 cans/minute), a highly destructive hidden landmine constantly troubles numerous OEM/ODM brand owners: the loss of control over filling precision.
Overfilling by just 1g across a million-level order will result in massive "Giveaway" cost losses; underfilling by 1g will trigger the strict net content sampling red lines of target markets (such as China NMPA, EU MID, US NIST), facing huge fines and mandatory delisting; and even a slight imbalance in the ratio of formula to propellant can turn the spray into a "water column" or cause internal pressure imbalance leading to "can bursting." As a professional cosmetics R&D and manufacturing factory, we know deeply that locking the filling error of gas-liquid two-phase fluids strictly within ±0.5g or even ±0.2g is never reliant on workers' "hand feel," but an extreme engineering project involving fluid dynamics, servo mechanics, and Statistical Process Control (SPC). Today, we will deeply dissect the underlying control logic of Sunscreen Spray Filling Precision, helping your brand build a dual moat of cost and compliance.
Scientific Root Causes: Why High-Speed Filling Easily Breaches the "±0.5g" Red Line
The filling of sunscreen sprays is far more complex than ordinary lotions. The root causes of precision loss mainly lurk in the following three physical and mechanical blind spots:
Blind Spot 1: Fluid Dynamics Disturbance and "Water Hammer Effect"
Sunscreen formulas usually have high viscosity or contain suspended powders, while propellants (like LPG, DME) are low-boiling-point fluids that vaporize extremely easily. The moment they are injected into the can at high pressure and speed, the fluid generates intense turbulence and cavitation. If the filling valve does not open and close smoothly, the fluid impacting the bottom of the can or the liquid surface will create a "Water Hammer Effect," causing fluid splash-back or volume expansion, making the actual injected mass fluctuate violently and ruining Sunscreen Spray Filling Precision.
Blind Spot 2: Mechanical Stress Deviation in Valve Crimping
The sealing core of an aerosol lies in the crimping of the valve cup and the can finish. If the downward pre-tightening force of the crimping equipment is uneven, or if the wear of the crimping claws causes micron-level deviations in the Crimping Diameter and Crimping Depth, it will not only cause chronic micro-leakage of the propellant during subsequent storage (leading to a reduction in total weight) but might also crush the valve stem, making it impossible for consumers to press the product out.
Blind Spot 3: "Dynamic Weighing Drift" on High-Speed Lines
On a high-speed flow line running at hundreds of cans per minute, mechanical vibrations, airflow disturbances, and the inherent temperature drift of the sensors themselves will severely interfere with the signal acquisition of the weighing module. If static weighing or low-precision dynamic weighing is used, the system will generate a massive amount of "false rejects (killing qualified products)" or "missed judgments (releasing underweight products)."
Engineering Breakthroughs: The "Trinity" Control Matrix to Achieve ±0.5g Extreme Precision
To completely eliminate filling errors, our factory has comprehensively upgraded its aerosol and high-pressure spray filling lines in 2026, building a "trinity" closed-loop control system from fluid metering, mechanical crimping, to dynamic feedback for ultimate Sunscreen Spray Filling Precision.
Strategy 1: Coriolis Mass Flow Meter and Two-Stage Filling
We have completely abandoned traditional "volume filling" or "time filling" methods, fully introducing industrial-grade, highest-precision Coriolis Mass Flow Meters.
Direct Mass Measurement, Ignoring Temp/Pressure Interference: This flow meter directly measures the "mass" of the fluid rather than volume, fundamentally eliminating metering errors caused by workshop temperature changes, formula density fluctuations, or pipeline pressure variations.
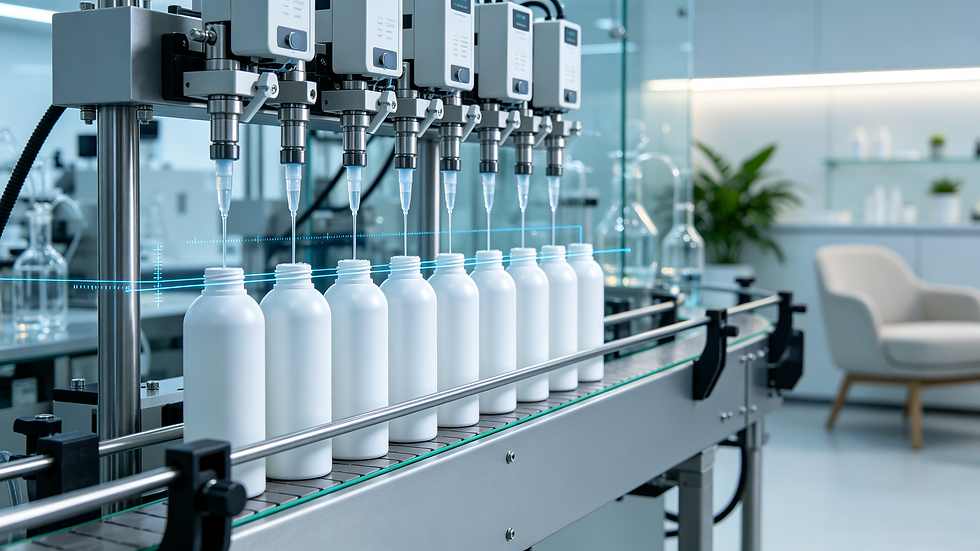
Two-Stage Closed-Loop Filling: The PLC system controls the filling valve to execute a "slow-fast-slow" three-stage curve. The initial slow speed prevents splashing, the middle high speed fills for efficiency, and the final ultra-slow "dribble feed" finishes the process. This fluid dynamics optimization completely eliminates the water hammer effect and dripping, locking the single fluid injection error within ±0.2g.
Strategy 2: Servo-Driven "Micron-Level" Valve Pre-tightening and Crimping Control
Crimping is the last physical defense line to lock in precision. We have eliminated traditional pneumatic crimping machines and adopted a fully Servo-driven Crimping matrix.
Precise Setting of Pre-tightening Force: The servo system can precisely control the torque and displacement of the crimping head pressing down, ensuring the valve base and can finish fit together with perfect pre-tightening force, neither damaging the sealing ring nor leaving micro-leak gaps.
3D Dimensional Online Monitoring: After crimping, laser displacement sensors immediately perform a 360-degree non-contact scan of the crimping diameter and depth for every can. Any defective product exceeding the ±0.05mm tolerance is instantly marked and rejected by the system, ensuring 100% mechanical sealing integrity.
Strategy 3: High-Precision Dynamic In-line Checkweighing and Automatic Compensation
After crimping and propellant gassing, the product enters the dynamic checkweighing stage.
Electromagnetic Force Compensation Sensors: We use electromagnetic force balance weighing sensors with extremely high anti-vibration capabilities, paired with digital filtering algorithms. Even when the line is running at high speed (up to 400 cans/minute), it still achieves a reading resolution of ±0.1g.
Feed-forward Compensation: This is the core soul of achieving ±0.5g Sunscreen Spray Filling Precision. The in-line weighing system does not just "reject defective products"; it feeds the weight data of every single can back to the front-end filling machine PLC in real-time. When the system detects a slight drift trend in weight (e.g., flow rate slowing down due to a drop in the formula tank liquid level), it will automatically fine-tune the opening time of the next can's filling valve (at the millisecond level), achieving zero error accumulation and nailing the overall batch precision firmly within the golden zone of ±0.5g.
SOP and QC Validation: Defending Batch Stability with Data
The limits of hardware require rigorous SOPs (Standard Operating Procedures) to escort. We have established a filling SOP system that complies with global metrology regulations:
1. First Article Inspection (FAI) and "Golden Weight" Calibration
Every time the machine is started, the line is changed, or the formula is switched, the operator must use "standard weights" certified by the national metrology institute to dynamically calibrate the in-line weighing system. Simultaneously, the first 10 cans are destructively disassembled to weigh the net weight of "empty can + valve," "formula," and "propellant" respectively. Mass production can only begin after signing off that the three-phase ratio 100% matches the BOM (Bill of Materials).
2. SPC (Statistical Process Control) and CPK Real-Time Monitoring
During mass production, the MES system automatically collects in-line weighing data and draws X-bar R (Mean-Range) control charts in real-time. The QC team focuses on monitoring the CPK (Process Capability Index). Our internal release red line is: the CPK for filling weight must be > 1.33 (even pursuing > 1.67). This means the natural fluctuation range of the production line is far smaller than the ±0.5g tolerance band, statistically eliminating the possibility of "short weight" or "overfilling."
3. Environmental Compensation and Scheduled Spot Checks
Drastic changes in workshop temperature and humidity, or direct blowing from air conditioning vents, will affect the zero point of high-precision sensors. The SOP strictly stipulates that the weighing module must have automatic temperature compensation, and every 2 hours, QC personnel must use a standard Test Piece for "blind spot checks" to verify the sensitivity and accuracy of the rejection pusher.
Compliance Claims and Business Empowerment: Precision is Profit, Precision is Safety
In the 2026 global regulatory and business context, the ±0.5g filling precision of Sunscreen Spray Filling Precision is not just a technical show, but tangible business empowerment:
Global Net Content Compliance (Legal Metrology Compliance): Ensures products perfectly pass the strict sampling inspections of China's "Measures for the Supervision and Administration of Quantitative Packaging Commodity Metrology," EU OIML R 87 / MID Directives, and US NIST Handbook 133, completely avoiding regulatory heavy fines caused by "exceeding negative deviations."
Eliminating Hidden Losses from "Giveaway": For brand owners with an annual output of tens of millions of cans, compressing the average filling surplus from +2g to +0.5g saves millions of RMB in expensive sunscreen formula and propellant costs annually, directly converting to the brand's net profit.
Locking Gas-Liquid Ratio and Explosion-Proof Safety: Precise filling ensures the absolute safety of the "Headspace" inside the can, maintaining the designed saturated vapor pressure, fundamentally eliminating the risk of can bursting in high-temperature transport or sun-exposed environments.
Conclusion: Reshaping the Certainty of Aerosol Manufacturing with Precision Engineering
The engineering control of Sunscreen Spray Filling Precision is a comprehensive test of a contract manufacturer's fluid dynamics application, servo automation integration, and statistical quality management capabilities. In the fiercely competitive global market, replacing extensive volume filling with the scientific system of "mass flow meter + servo crimping + dynamic feedback" is the only way for brand owners to guard the profit bottom line and avoid compliance risks.
Partner with Deva Skincare for Precision Sunscreen Spray Filling Precision & Zero-Defect Manufacturing
Are you looking for a reliable skincare factory that guarantees absolute filling precision (±0.5g) for your sunscreen sprays and aerosols?
Are you seeking a trusted partner to launch or scale your sun care line with state-of-the-art filling technologies that eliminate "giveaway" costs and ensure global legal metrology compliance? At Deva Skincare, we specialize in high-speed aerosol and pump-spray manufacturing backed by advanced engineering controls to ensure ultimate Sunscreen Spray Filling Precision.
Our production facilities are equipped with Coriolis Mass Flow Meters, Servo-driven Crimping systems with 3D dimensional monitoring, and Dynamic In-line Checkweighing with real-time feed-forward compensation. Governed by strict SOPs and SPC (CPK > 1.33) real-time tracking, we ensure every single can meets the exact formulation ratio, net weight, and safety standards required by global markets (NMPA, EU MID, FDA).
By collaborating with Deva Skincare, you gain access to industry-leading Sunscreen Spray Filling Precision, proactive cost optimization, and a resilient supply chain that protects your margins and brand reputation. Contact us today to discover how our precision engineering can help you succeed.


Comments